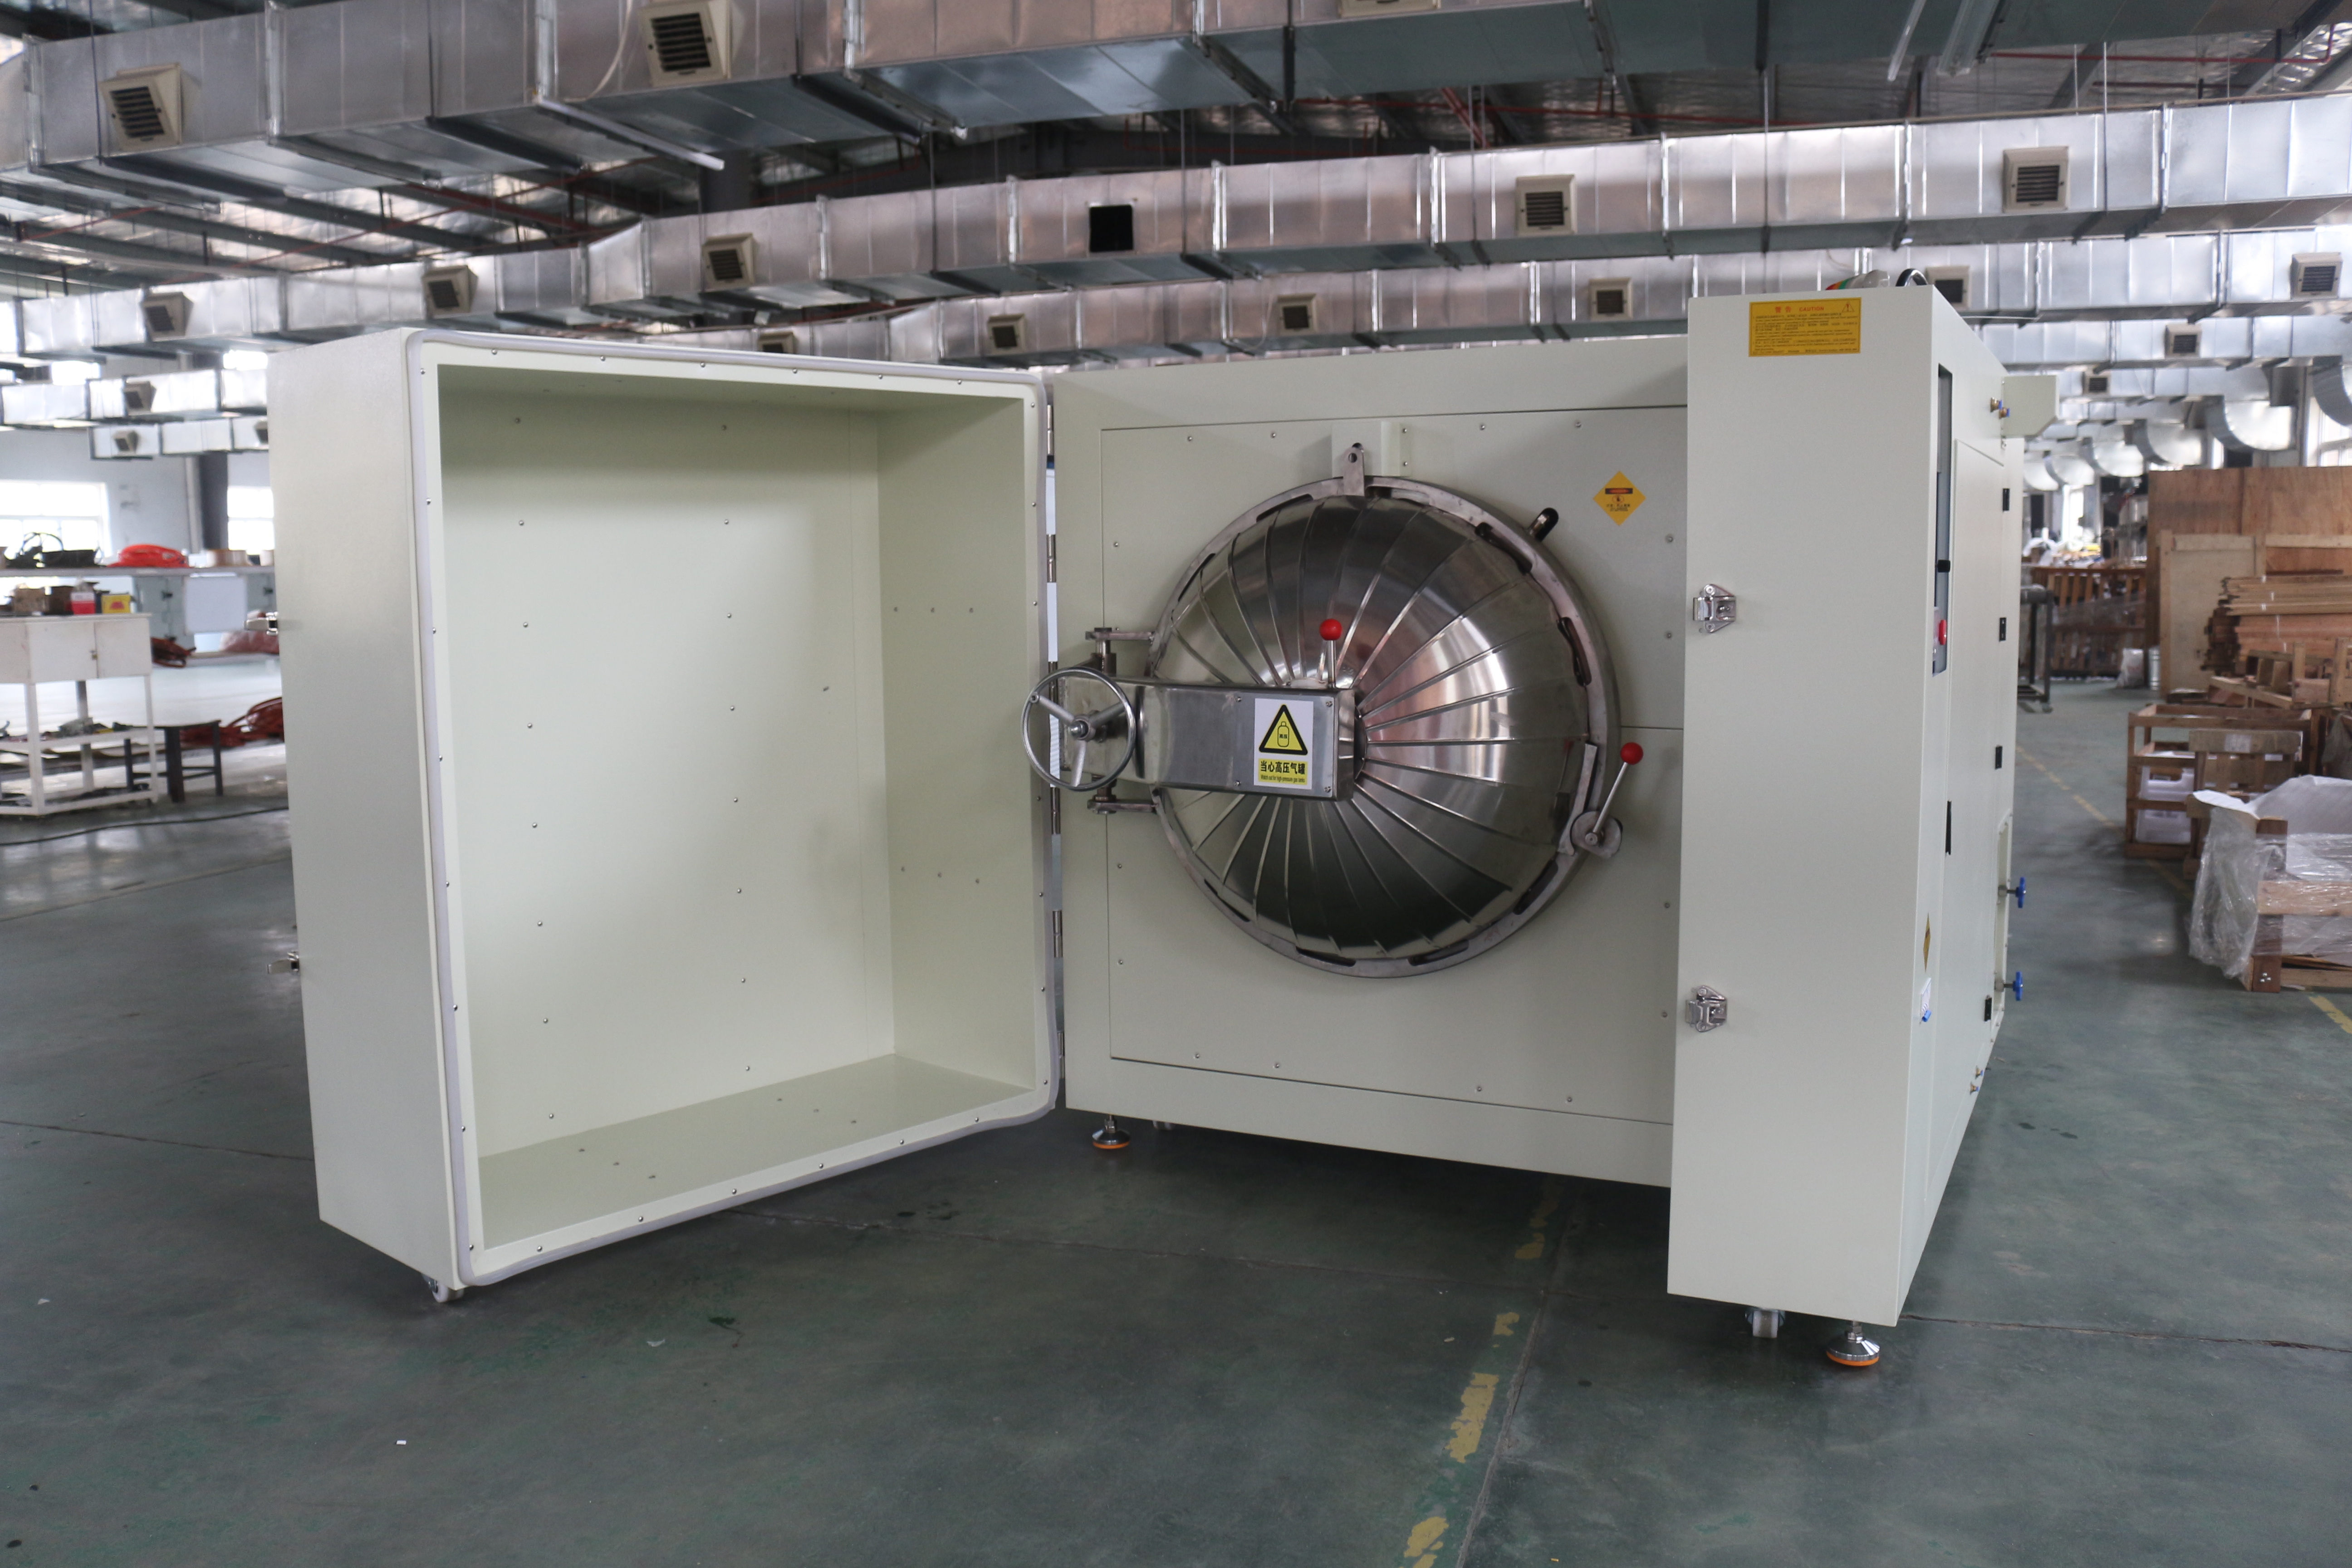
Validation plan for complete bubble removal with the Xinhai positive/negative-pressure die-bonding oven
Simplified DOE plan to verify complete defoaming on Xinhai positive/negative-pressure die-bond furnaces
1. Core objective
“ vacuum - - - ” = 0
2. Simplified variable design (focus on key factors)
and “ ”
Variable type
Variable name
Sample settings
Purpose (simulate different initial bubble risks)
Pre-treatment
Flux residue
① Uncleaned (high residue); ② Cleaned (low residue)
Verify how well the equipment removes bubbles from flux outgassing
Pre-treatment
Residual moisture in the substrate
① not pre-baked (high moisture); ② 150 °C / 60 min (low moisture)
Verify how well the equipment removes bubbles from evaporating moisture
Underfill properties
Adhesive flowability
① High viscosity (traps bubbles); ② Low viscosity (easier degassing)
Verify how well the equipment removes bubbles trapped by capillary flow
3. Test steps matched to the Xinhai process flow (core validation logic)
Strictly follow the user process flow and clarify how each step relates to defoaming:
vacuum 100Pa 10
Role: oxygen purge + initial removal of free bubbles (surface and shallow).
hot-air 100℃ Tg 1.5
Purpose: use adhesive flow so trapped micro-bubbles rise / gather (prep for later degassing).
vacuum + → 100℃ 30
Role: with vacuum + temperature control, remove ~90% of bubbles (including those from flux and moisture).
5kg / cm² → 150℃
Purpose: high pressure compresses the remaining micro-bubbles, and curing then locks in the bubble-free state.
“ ”
“ + ”
SAT ultrasonic scanning (C-SAM) / X-ray: inspect every sample to confirm there are no internal voids (including at the chip-substrate interface and inside the adhesive layer).
Cross-section microscopy (200-500x): from SAT-pass samples, randomly take 3 slices and count bubbles (requirement: bubble count = 0).
5. Validation logic for the test conclusions
If all variable combinations (3 variable types x 2 sampling = 8 runs, 6 pcs each) pass the above flow and meet:
No bubble signal of any kind in the SAT images;
Cross-section observation: bubble count = 0;
“ vacuum - - - ”
hot-air oven hot-air vacuum oven vacuum oven “ vacuum - hot-air - vacuum and - ”